
- Sourcing CNC machining? The test is not the tolerance printed on a brochure — it is whether the shop can hand you a CMM report for the exact feature you are buying, with the band, the sample size and the study window all named.
- What CNC machining is: a subtractive process — a cutter removes material from a workpiece along a programmed toolpath until the geometry, tolerance and surface finish on the drawing exist.
- Over 100 machines on one floor — Mazak / Brother / Tsugami / Star / Citizen class across 6,800 m², with 50+ 3-axis, 20+ 4-axis, 20+ 5-axis, 25+ lathes, 7+ grinders and 20+ inspection instruments.
- Held tolerances: ±0.003 mm on milling, ±0.002 mm on turning, ±0.002 mm on grinding, each checked on Hexagon CMMs. Capability is stated per characteristic — Ppk ≥ 1.67 initially and Cpk ≥ 1.33 in production for key and special characteristics (≥ 1.33 general). Each report lists the feature, band, sample size, sigma method and study window.
- ISO 9001:2015 · IATF 16949:2016 (design excluded) · ISO 14001:2015 — held by Dongguan Zhuohang Ltd, the entity that invoices you.
- Order terms: MOQ 1 piece, lead times of roughly 3 / 7 / 30 days depending on complexity.
- Build-to-print; Ppk ≥ 1.67 initial critical, ≥ 1.33 general.
What actually changes between low-volume and high-volume machining?
The part does not change; the economics around it do. At one piece, the setup and first-article dominate the cost. At ten thousand pieces, setup is amortized and material, cycle time, and yield dominate. The same drawing can be profitable at both ends only if the shop runs them on one balanced line instead of treating prototypes and production as separate worlds.
We run more than 80 machines (Mazak, Brother, Citizen, Star, Tsugami) under one roof, so a prototype insert and a production lot compete for the same capacity on purpose. That is what lets a single part scale without re-qualifying a new supplier.
The distinction matters because if you price a part at one volume and buy it at another, you are paying for the wrong cost structure. A prototype quote applied to a production order is a markup you never needed; a production quote applied to a bridge order is a minimum you cannot sell. The rest of this page is about reading the two structures separately so the number you pay matches the quantity you actually need.
Why does MOQ 1 piece matter for you?

An MOQ of 1 piece means you can validate a design with a real machined part before committing to volume, instead of betting on a render. You find the tolerance problem, the material call, and the fit issue on part one, not on part five thousand. It also means a bridge order between production runs costs you a setup, not a minimum batch you cannot sell.
For a hardware founder or NPI engineer, MOQ 1 is risk control. It turns a blind production commitment into a staged one, and the staged path is cheaper when the design is still moving.
A large MOQ is, at its core, a way for a shop to hide its setup cost inside a forced batch. The shop does not want to sell one part because one part exposes the setup for what it is — a large fixed cost carried by a single unit. By insisting on MOQ 1, you are insisting that the supplier show the setup separately and let you decide when it is worth amortizing. That transparency is the difference between buying a part and buying a minimum you were talked into.
What is a CNC machining company?
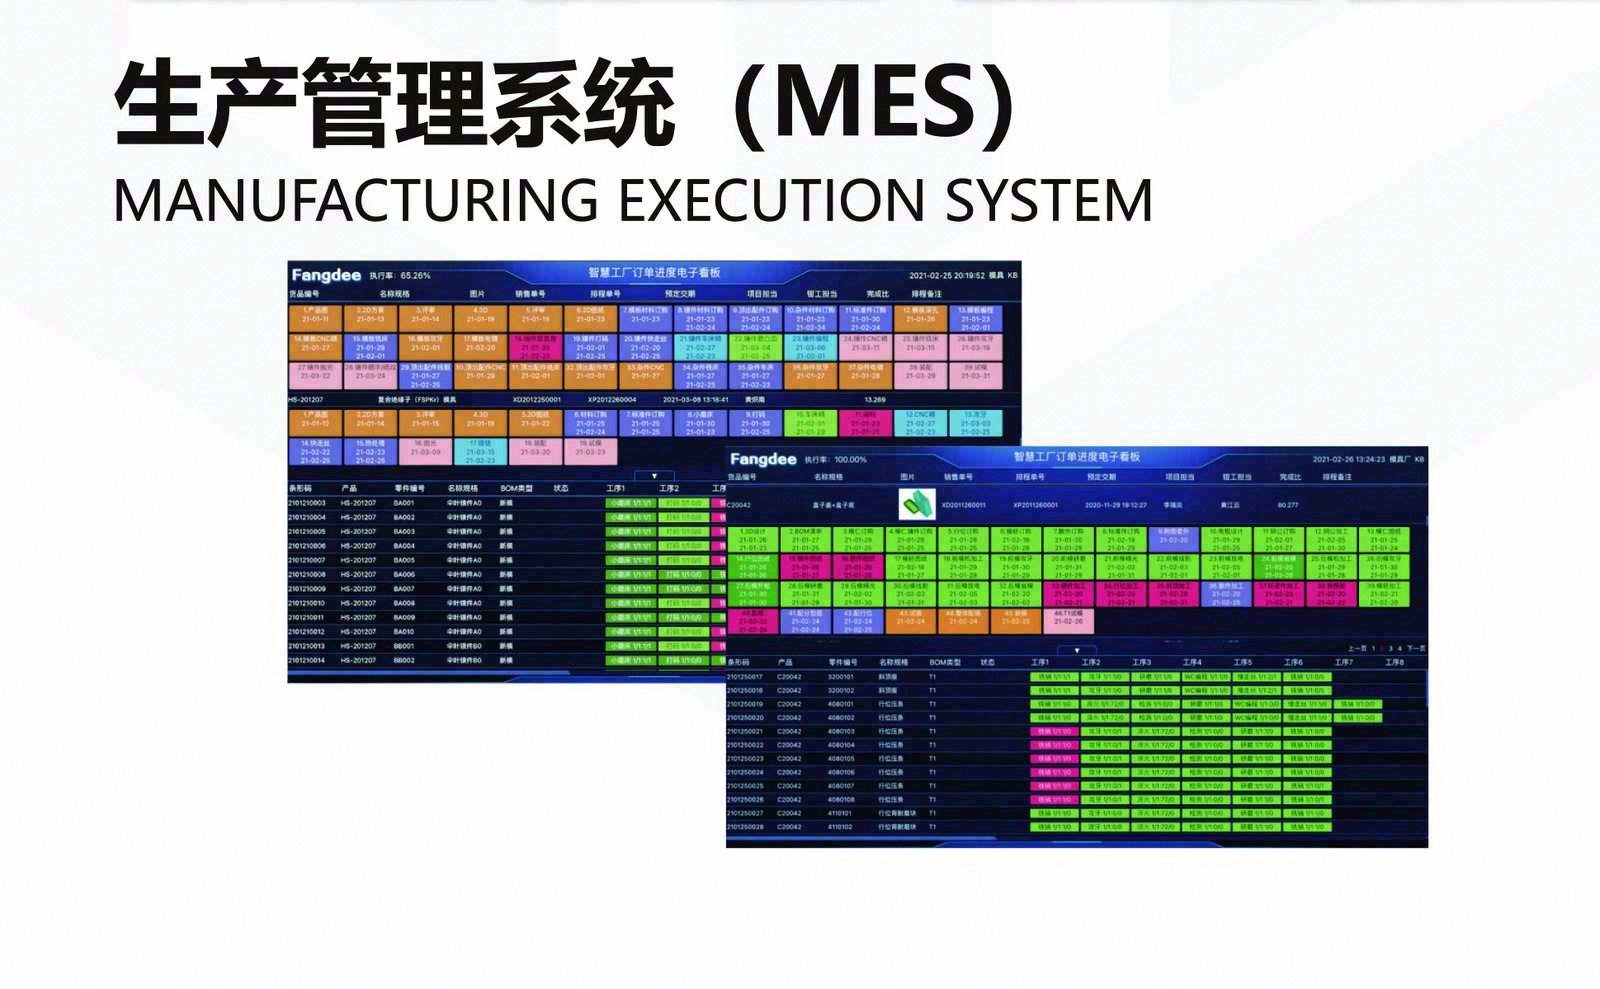
A CNC machining company is a machining business that operates computer-numerically-controlled milling, turning, and grinding equipment to produce parts against a customer drawing. The company's scope is broader than a broker: it runs end-to-end from raw material (bar stock, plate, cast blank) through machining, surface treatment, inspection, packaging, and export, with the certifications (ISO 9001 / IATF 16949 / ISO 14001) that support export to U.S., EU, and Asian automotive and industrial buyers.
The discipline at company scale separates into milling lines (3-axis, 4-axis, 5-axis machining centres), turning lines (CNC lathes and Swiss-type lathes with bar feed), and finishing lines (precision surface grinding, cylindrical grinding, wire EDM, anodising, powder coat, plating). A CNC machining company is distinguished from a broker by integrated quality systems (calibration, SPC, MSA, PPAP, IMDS) and by the certifications that allow direct shipment to automotive and aerospace buyers.
The output of a CNC machining company is a part that meets the drawing — geometry, tolerance, surface finish, and material certificate — and is documented to a quality plan (FAI, PPAP, IMDS) plus the export paperwork (Certificate of Origin, mill certificate, REACH/RoHS declarations). That is the answer to "what is a CNC machining company": a machining business that runs CNC machining end-to-end, with the certifications and documentation that let the part land in the destination country.
What dominates cost at high volume?
At volume, cycle time, material yield, and scrap rate take over. Process choice matters: a 5-axis setup that looked expensive at one piece can beat three operations at ten thousand because it removes fixtures and handling. Tool life, coolant, and inspection sampling also scale with the count, so the economic process is not the one that was cheapest to start.
This is where Cpk earns its keep. Holding Ppk ≥ 1.67 at the initial study on critical characteristics and Cpk ≥ 1.33 in production on general characteristics means scrap stays low at volume, and low scrap is the largest single driver of unit cost once the setup is paid.
A useful mental model is to split a batch into three layers. The setup layer is fixed and shrinks per piece as quantity rises. The cycle-time layer is constant per piece and never shrinks — it is the floor. The yield layer is the variable that quietly grows when the process is not capable, because every scrap part is a piece you paid to make and cannot sell. The supplier that wins your volume order is not the one with the lowest cycle-time quote; it is the one whose yield layer stays flat as the count climbs.
How do you scale from prototype to production smoothly?
Keep the same supplier and the same drawing release. We are build-to-print, so the first machined part becomes the measurement baseline; the production lot is judged against it. The program, the fixture concept, and the inspection plan carry over, which removes the re-qualification step that breaks most scale-ups.
Lead time scales with complexity: 3 / 7 / 30 days for simple / standard / complex work. Plan the prototype against the same ladder so the production number is a known quantity, not a surprise.
The hidden risk in scaling is the re-qualification hand-off. If the prototype shop and the production shop are different companies, the second shop re-learns the part from scratch: new program, new fixture, new first article, new scrap. That re-learning is exactly the cost you thought you had already paid. Keeping prototype and production on one floor — and on one quality system — is what lets the first article carry its value forward instead of being thrown away.
The first article is the cheapest failure you will ever buy, because it fails on one part instead of a thousand. When you release a production run on an unvalidated process, every defect is multiplied across the batch — a tolerance drift caught at part one costs a scrap bin; caught at part one thousand costs a line stoppage and an air-freight replacement. A proper first article ships with a measured dimensional report against your drawing, so the production run becomes a reproduction of an approved part rather than a bet.
How does process choice change with volume?
At one piece, choose the process that proves the design: often 3-axis plus a second op. At volume, choose the process that minimizes total handling: 5-axis or mill-turn that consolidates setups. We will tell you when the expensive machine lowers total cost at your quantity, and when it only adds cost. The right answer moves as the volume moves.
| Process | Low volume (1–10 pcs) | High volume (1,000+) |
|---|---|---|
| 3-axis milling | Default; fast to program, simple fixture | Worth it only if the part stays on one face |
| 4-axis / 5-axis | Justified when faces must relate | Removes re-fixturing on every unit |
| Mill-turn | Justified for tight shaft interfaces | Consolidates lathe + mill into one setup |
| Grinding | Only if the drawing demands the finish | Keeps the tightest dimension in-house |
The table is a guide, not a rule. The correct process is the one that minimizes the sum of setup and cycle time at your quantity, and that sum has to be computed, not assumed. A shop that always recommends 5-axis, or always recommends 3-axis, is pricing its preference, not your part.
Where does the break-even between setup and cycle time actually fall?
There is no universal quantity where setup stops mattering; the break-even is the point where one more part costs more in machine time than the remaining share of the setup. That point moves with the part. A complex part with a long setup and a short cycle crosses over early; a simple part with a short setup and a long cycle crosses over late.
Think of it as two lines on a graph. Setup is a flat line that starts high and is divided by quantity, falling toward zero. Cycle time is a flat line per piece that never moves. Where the falling setup line dips below the cycle-time line is the crossover. Before it, you are mostly paying for the learning; after it, you are mostly paying for the metal and the machine time.
The practical test is the second order. If the first order carries the setup and the second order reuses the program and fixture, the second order should sit close to the cycle-time floor. If the shop quotes the second order at near-first-order price, it is charging you for the learning twice, and the break-even math no longer works in your favor.
What does the cost-per-part curve look like from one to ten thousand?
The curve is not a straight line; it is a falling curve that flattens. At the far left, one part carries the whole setup. As quantity rises, the setup divides across more units and the per-part cost drops steeply. As the count climbs further, the drop slows, because the setup share is already small and what remains is cycle time and material, which do not fall with quantity.
| Quantity | Dominant cost driver | What you are really paying for |
|---|---|---|
| 1 | Setup and first article | The learning: program, fixture, proof |
| 10 | Setup still visible | Learning plus the first few cycles |
| 100 | Cycle time rising | Machine time and tool wear |
| 1,000 | Cycle time and yield | Steady-state speed and scrap rate |
| 10,000 | Material and yield | Stock cost and the cost of every bad part |
The table explains why quoting is a volume question, not a geometry question. Send the same drawing with two different quantities and a competent shop returns two different cost structures. If a supplier quotes the same structure at both quantities, it has not priced the part — it has priced a guess.
How does material choice interact with volume?
Material sets two costs at once: the stock price and the machining speed. A grade that cuts fast and sheds heat well is cheap per part even at tight tolerances, because the spindle runs fast and the tool lasts. A grade that work-hardens or retains heat is expensive per part, because the feed slows and the tool wears, and that penalty repeats on every unit of a production run.
| Material | Machining behavior | Per-unit cost effect at volume |
|---|---|---|
| 6061-T6 aluminum | Fast feeds, good heat dissipation | Low; the default for prototypes and housings |
| 7075-T6 aluminum | Slightly slower than 6061, high strength | Low to mid; pay a little more for strength |
| 5052 aluminum | Gummy, lower machinability | Mid; chosen for corrosion and forming, not speed |
| 303 stainless | Free-machining, breaks chips cleanly | Mid; the fast route through stainless |
| 304 / 316 stainless | Work-hardens as it cuts, slow feeds | High; corrosion resistance costs machine time |
| 4140 alloy steel | Moderate, hardens after heat treatment | Mid to high; strength at the cost of tool life |
| Brass (C360) | Chips break cleanly, fine threads run fast | Low; the reference many shops measure against |
The lesson is the same one that runs through this whole page: pick the grade that earns its keep. A drawing that calls for 316 where 303 would function is paying for corrosion resistance the part never uses, and paying for it in machine time across the entire run, not just in stock. At volume, that choice is multiplied by the count, which makes material selection the single quietest cost lever you have.
Strength is the other half of the decision, and it is a published number rather than a judgment call. An aluminum 7075-T6 part carries roughly 503 MPa of yield strength against 276 MPa for 6061-T6, which is why the aerospace and robotics work pays the slightly slower machining. An alloy steel 4140, quenched and tempered, reaches about 655 MPa and still machines reasonably. The table below is the short version buyers ask for, and it is why the grade on the drawing is a property decision first and a cost decision second.
| Material (condition) | Typical yield strength | Why you choose it |
|---|---|---|
| 6061-T6 aluminum | ~276 MPa | Machines fast, anodizes well, general mechanical parts |
| 7075-T6 aluminum | ~503 MPa | High strength-to-weight for load-bearing parts |
| 5052-H32 aluminum | ~193 MPa | Corrosion and forming, where strength is secondary |
| 304 stainless (annealed) | ~215 MPa | General corrosion resistance, work-hardens as it cuts |
| 316 stainless (annealed) | ~290 MPa | Marine and chemical resistance, molybdenum added |
| 4140 alloy steel (QT) | ~655 MPa | High strength for shafts, fasteners, tooling |
How do tolerances move the price at each volume tier?
A tolerance is a cost instruction, not a quality statement. The tighter the tolerance, the more careful the process, the more inspection it needs, and sometimes the more finishing steps it forces. A drawing that stamps a tight tolerance on every feature is instructing the shop to spend money on dimensions that do not matter, and to carry that spend across every part of the run.
General tolerances cost less than specific ones. A drawing that says "ISO 2768-m" hands the shop a standard band — fine (f), medium (m), or coarse (c) — and lets it machine to the band without over-processing. A drawing that calls out a tight positional tolerance on a specific feature reserves the precision for the one place it matters. The difference in cost between those two drawings can be large, and it repeats on every unit.
| Tolerance approach | Cost effect | When to use it |
|---|---|---|
| ISO 2768-c (coarse) | Lowest; standard stock removal | Non-critical features, clearance fits |
| ISO 2768-m (medium) | Mid; standard machining | General mechanical features |
| ISO 2768-f (fine) | Higher; careful process control | Fit-critical and locating features |
| Tight specific callouts | Highest; extra inspection, maybe grinding | The few features that must mate precisely |
your discipline is to put tight tolerances only where function requires them, and to leave everything else on a general band. That is not a shortcut; it is how the drawing tells the shop where the value is. At volume, the saving from reserving tolerance compounds across the batch, because every over-processed feature is time you paid for on every single part.
When does 5-axis or mill-turn beat 3-axis as volume climbs?
The break happens when the cost of re-fixturing a 3-axis job exceeds the cost of running a 5-axis or mill-turn setup. At one piece, a second operation is cheap — a fixture, a flip, a re-indicate. At ten thousand pieces, that flip happens ten thousand times, and every flip is a chance to lose alignment and add handling.
5-axis removes the flips. A part with features on five faces can be machined in one or two setups instead of five, so the tolerance relationships hold and the part spends less time in handling. Mill-turn does the same for parts that mix turning and milling, keeping the interfaces concentric because the part never leaves the chuck.
The trap is pricing the machine, not the part. A 5-axis hourly rate looks expensive until you add up the fixtures, the deburr steps, and the handling it removes at volume. The opposite trap is staying on 3-axis past the point where re-fixturing costs more than the upgrade. The honest shop computes the crossover for your quantity and tells you which side you are on, and that number is what you are paying for when you send a drawing with a volume.
How does scrap rate and Cpk compound at volume?
At one piece, a 1% scrap rate is an abstraction. At ten thousand pieces, it is one hundred parts you paid to make and cannot sell, plus the freight and duty on them, plus the time lost finding them. Scrap is the one cost that multiplies with quantity without giving you anything in return, which is why process capability is the central cost lever at the production end.
Cpk is the number that predicts scrap. A process holding Ppk ≥ 1.67 at the initial study on key characteristics sits comfortably inside its tolerance band, so almost nothing falls out of spec. A process at Cpk 1.0 sits right on the edge, so natural variation keeps spilling parts out, and those parts become your cost. On a representative length characteristic, our SPC shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim), comfortably inside the target.
One more check on that number: the 0.4 mm band behind it is wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright, so read this figure as evidence about one characteristic on one run, not as a blanket tolerance claim.
Ask a supplier for a Cpk study from a job like yours, and read the sample size it is built on. A number copied from a handbook means nothing; a study from a real job, with a named characteristic and a stated sample size, is the closest thing machining has to a forward price on your scrap bill.
Sampling is the second half of the same discipline. At one piece, every part is measured; at ten thousand, no shop measures every part, so the question becomes what the sampling plan catches. A control plan that names the critical characteristics, the sampling frequency, and the reaction when a point drifts is the difference between catching a shift early and discovering it in your incoming inspection. The method stays constant from part one to part ten thousand; only the sampling plan changes.
What DFM decisions reduce setup and cycle time at both ends?
Design for manufacturing is where a part's cost is fixed before any metal is cut. Three rules do most of the work. First, leave internal corners radiused rather than sharp, because a round tool cannot cut a square inside corner — a radiused corner drops out of the same tool path, while a sharp one forces an EDM step or a smaller, slower tool. Second, keep hole depth within about four to five diameters before special tooling. Third, put threads and tolerances only where they function, so the shop does not spend machine time on features that will never be measured in service.
- Radiused internal corners: match the corner to the tool radius; it avoids a second slow pass.
- Hole depth within 4–5× diameter: deeper needs special tooling and slower pecking.
- Wall thickness above the floor for the material: too-thin walls chatter and deflect.
- Fewer setups by design: features on one face mean one fixture, one indicate, one risk.
- Standard stock sizes: a blank that starts near net shape wastes less and cuts faster.
Each rule lowers cost at every volume, but they matter most at the two ends of the curve. At low volume, DFM cuts the setup and the risk of a bad first article. At high volume, it cuts cycle time and scrap, and those savings compound across the whole run. The cheapest part is the one designed to be cheap before it ever reaches a machine.
How do surface finishes change the economics as volume grows?
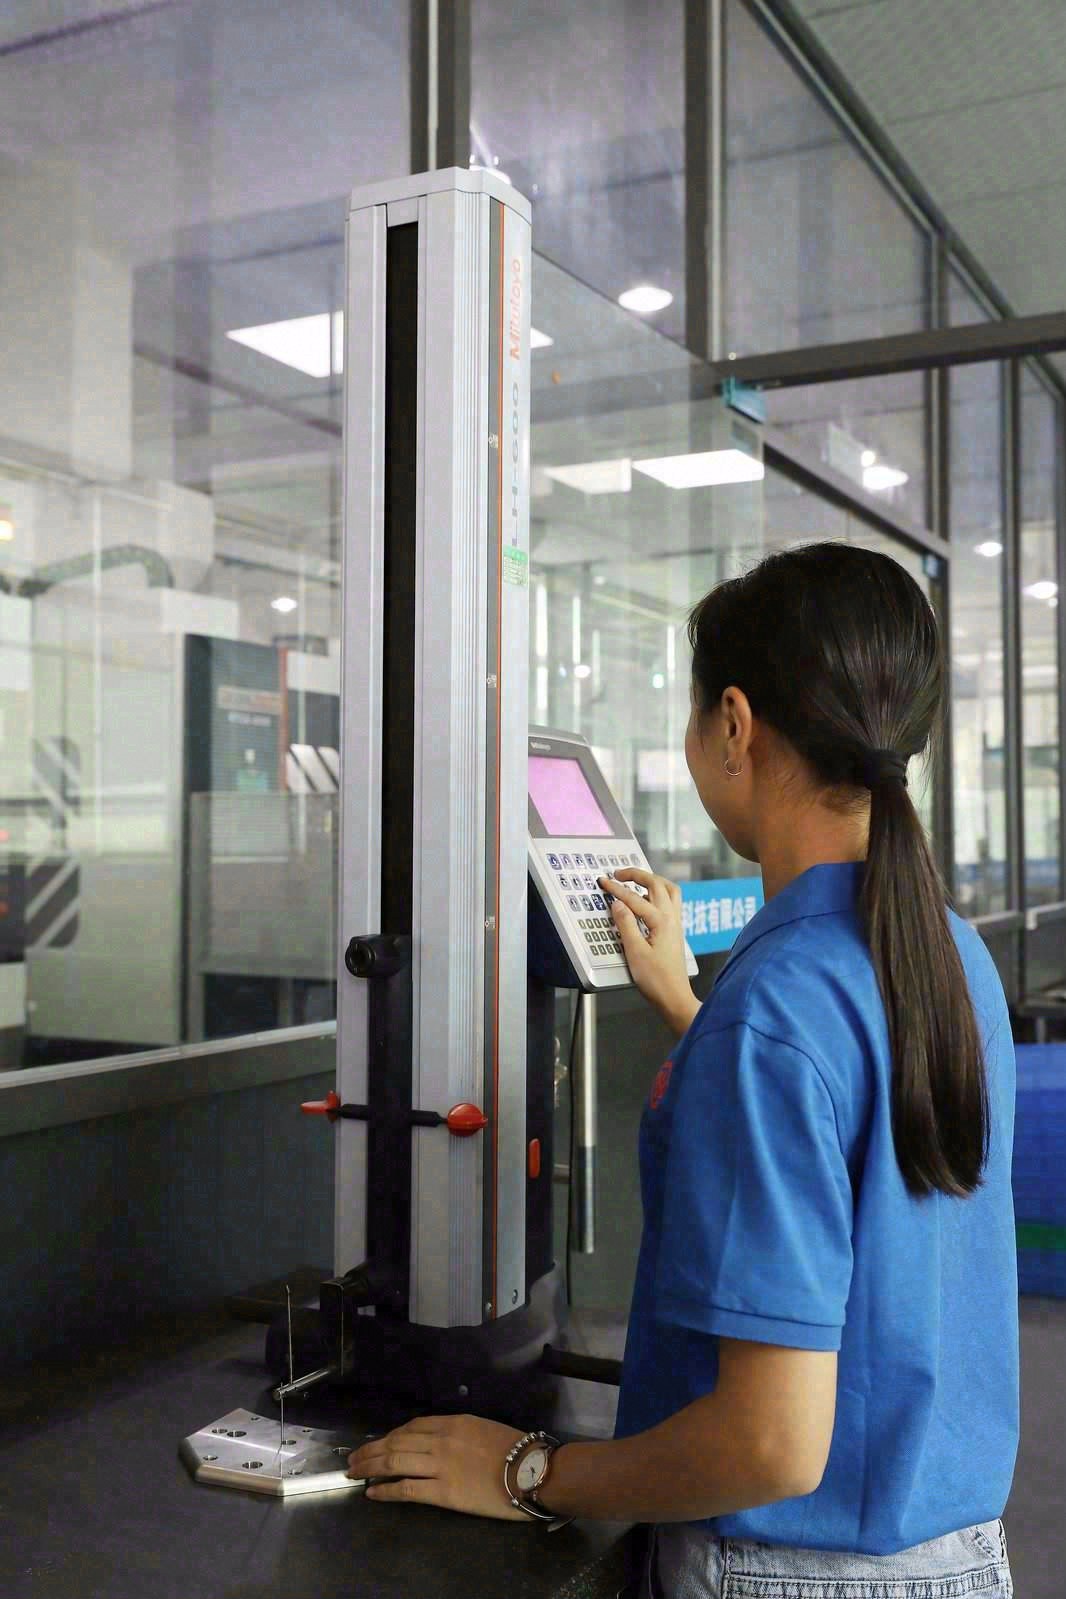
A machined surface already has a roughness set by the tool and the feed. Asking for a finer finish than the function needs adds a finishing step — grinding, lapping, or a secondary process — and that step adds cost on every part. Surface finish is a ladder, and each rung costs more than the one below it.
| Surface finish (Ra) | Typical process | When it is worth the cost |
|---|---|---|
| 3.2 µm | Standard milling / turning | General surfaces, non-sealing |
| 1.6 µm | Fine milling / light grinding | Bearing seats, sealing faces |
| 0.8 µm | Precision grinding | Rotating fits, sliding surfaces |
| 0.4 µm and below | Lapping / polishing | Optical or metrology-grade surfaces |
Secondary finishing — anodizing, plating, passivation — scales the same way. It is a per-part cost, so it is invisible at one piece and a major line at ten thousand. The discipline is to specify the finish the function needs and nothing finer, and to decide whether the finish runs in-house or through a named partner before the volume exposes the difference.
How do Incoterms and logistics change the landed cost at volume?
The price on the quote is not the price at your dock. The gap between the two is filled by the Incoterms rule you agree to, which decides who pays for freight, insurance, and import clearance, and therefore who carries the risk while the parts are in transit. The rule matters more at volume, because the freight and duty scale with the order value.
- EXW (Ex Works): you take everything from the factory gate — freight, export, and import.
- FOB (Free on Board): the seller clears export and loads; you take risk from the port onward.
- CIF (Cost, Insurance, Freight): the seller pays freight and insurance to the destination port.
- DDP (Delivered Duty Paid): the seller delivers cleared, with duty paid, to your door.
None of these changes the machining cost, but each changes the total you actually pay. Two suppliers quoting the same part price under different Incoterms are quoting two different totals. When you compare volume quotes, compare them on the same term — otherwise you are comparing a factory-gate number against a delivered one and calling it a saving.
The practical move is to fix the Incoterms term before you compare prices, the same way you fix the material grade and the quantity. A fixed term, a fixed grade, and a fixed quantity turn two supplier quotes into two prices for the same thing, and only then is the cheaper number actually cheaper. Leave any of the three floating and you are comparing three different parts at three different prices while the spreadsheet pretends they are one.
What breaks the low-versus-high-volume math?
The math assumes three things hold: the setup is real and stated, the cycle time is the steady-state time, and the scrap rate stays where the Cpk says it will. When any of those fails, the per-part curve stops being the bargain it looked like. The failure shows up in a few recognizable ways.
- A setup hidden inside a minimum batch. If the quote has no separate setup line, you are being sold volume to bury the fixed cost.
- A process that was never right for the volume. Staying on 3-axis past the crossover, or jumping to 5-axis before it, both overpay.
- A scrap rate the supplier will not show. If there is no Cpk study, the yield layer is an unknown you are about to pay for.
- A tolerance callout on features that do not mate. Over-processed features are money spent on every part.
- A material grade that was never confirmed. A substituted alloy machines differently and fails differently, at your cost.
The counter-move is the same for each: ask to see the setup line, the process recommendation, the Cpk study, the drawing review, and the material certificate. A supplier that can show all five has a cost structure you can actually read; a supplier that cannot is asking you to trust a number it will not open.
How do you read a volume-tiered quote and challenge it?
A quote matched to volume is a document, not a single number. The useful quote separates setup from piece price, names the process it assumes at your quantity, states the material grade, and gives a lead time from the 3 / 7 / 30 day ladder. If any of those is missing, the quote is a guess wearing a number.
- Is setup a separate line? If not, ask why the fixed cost is buried.
- Does the process match the volume? Ask what changes at your real annual quantity.
- Is the material grade named? "Aluminum" is a family, not a grade.
- Is the lead time a commitment or a hope? Ask which tier the part lands in.
- Is there a Cpk or inspection plan behind the tolerance? A tolerance without measurement evidence is a wish.
Run those checks and the weak quotes fall apart on their own, because their cost structure was never real to begin with. The quotes that survive are the ones whose volume economics you can verify before you commit a dollar, which is the whole point of buying on the low-versus-high-volume logic instead of on the bottom line alone.
How does the same part cost differently across industries?
Volume economics do not play the same in every industry, because the order profile and the risk tolerance differ. An e-bike drivetrain maker runs medium batches of a part whose tolerance matters for quiet, reliable shifting — the cost question is how much scrap the supplier can prevent across a recurring lot. A robotics startup orders in ones and tens while the design is still moving, so MOQ 1 and fast first articles matter more than the per-piece floor. A medical device program runs low volume under heavy documentation, so the cost sits in traceability and inspection rather than in cycle time. A semiconductor equipment maker machines small batches of high-value parts where one scrap part costs far more than the stock, so process capability dominates everything else.
The common thread is that each industry sits at a different point on the same curve. The buyer who knows where their program sits — prototype, bridge, or steady production — can ask for the right cost structure instead of accepting the one a general-purpose shop happens to quote. The curve is the same everywhere; the point on it is yours.
How do you choose the right order quantity?
Order quantity is a balance between the setup you amortize and the inventory you carry. Buy too few and every reorder pays a fresh setup, so the per-part cost stays high. Buy too many and you tie up cash in parts you have not sold, on a design that may still move. The sweet spot is the quantity where the setup savings are captured without buying inventory the market has not asked for.
The MOQ sets the floor, not the target. A MOQ of 1 lets you buy the smallest batch that is sensible — a prototype, a bridge order, a first production lot. The larger, well-planned run then captures the setup savings on the parts you are confident in. Volume is how you buy the same part cheaper; validation is how you avoid buying the wrong part in volume. The two are separate decisions that the same quote should let you make separately.
What does the second order cost, and why does it matter?
The first order pays for the learning: the setup, the tooling, the program that turns your drawing into chips. The second order should cost less, because that learning is already banked. The difference between a shop that reproduces the first part exactly — same fixture, same program, same inspection plan — and one that treats every reorder as a fresh start is the difference between a flat per-part cost and one that keeps paying for the setup forever.
A shop that keeps your fixture, your program, and your inspection plan on file reproduces the part without re-learning it, so the per-part cost stays flat and the lead time stays short. A shop that loses that continuity charges you for the learning again, either in the price or in a slower ramp and the scrap that comes with it. When you compare suppliers, ask what happens on the second order — the answer is a forward price on your future batches, and it belongs on the same ledger as the cost of switching.
How does lead time interact with volume?
Lead time is set by complexity, not by a blanket promise. Our ladder is 3 / 7 / 30 days for simple / standard / complex work, and it applies the same way at one piece as at ten thousand, because the limiting step is the number of process steps, not the count. A part with surface finishing or ten to twenty operations lands in the longer tier whether you order one or a thousand.
The volume economics interact with the calendar in one specific way: an expedited order is a second setup you were not planning to pay. When a batch runs late and forces an air-freight replacement, you pay a fresh setup, a rushed schedule, and premium freight — all of which sit on top of the price you negotiated. A lead time you can trust protects your assembly schedule, and a protected schedule is itself a cost saving, because the expedite you never need is the cheapest one there is.
How do you spec a drawing for the volume you will buy?
The drawing is a cost document before it is a geometry document, and it should be written against the volume you intend to buy. Three habits do most of the work. First, tolerance only the features that mate — leave everything else on an ISO 2768 general band. Second, name the material as a grade, not a family, so the shop prices the alloy you actually want and verifies it by XRF against the mill certificate. Third, send the STEP or IGES model with the 2D drawing, so the programming does not have to guess a dimension.
Each habit removes a place where cost hides. A vague drawing returns a range, not a price, because the shop has to guess the tolerance, the grade, and the geometry. A precise drawing returns a firm number the shop can honor, and, at volume, a firm number that holds across the whole run instead of drifting with every assumption the shop had to make. The drawing is the cheapest place to remove cost, because everything downstream follows from it.
How do you compare two suppliers on volume economics?
Two suppliers quoting the same part rarely carry the same cost structure, and the bottom-line number hides the difference. The fair comparison adjusts each quote for what the process will actually deliver: the scrap the Cpk predicts, the lead time you can hold someone to, and the second-order price once the setup is amortized. A supplier that buries the setup, skips the process recommendation, and quotes no Cpk study is offering a price with an unknown attached.
| Signal | What it tells you |
|---|---|
| Setup and piece price as separate lines | The fixed cost is real and visible, not buried in a minimum |
| Process named for your quantity | The shop computed the crossover, not its preference |
| Cpk study from a real job | The scrap layer is measured, not assumed |
| Material grade + mill certificate | The alloy you pay for is the alloy you get |
| Lead time tied to the 3 / 7 / 30 ladder | The schedule is a plan, not a hope |
Run the two quotes through that table and the cheaper one often stops looking cheap, because its risk was never priced in. The suppliers that survive the table are the ones whose volume economics you can see, which is the only basis on which a low-versus-high-volume decision should ever be made.
What should you send to get the volume economics right?
Send the drawing, the material, the tolerance, and your expected volume and cadence (one-off, bridge, or steady production). We return a price that separates setup from piece cost and names the process we recommend at your quantity, with lead time from the 3 / 7 / 30 day ladder. Email [email protected] or call +86 13126536955.
The more of the volume picture you send, the more honest the number that comes back. A drawing with a quantity is a guess; a drawing with a quantity and an annual volume is a plan. Send both, and the quote you get is matched to the cost structure you will actually live in, not the one a shop assumed you wanted.
The volume is not an afterthought on the RFQ; it is the variable that decides which cost structure applies. Name it up front, and the setup, the process choice, and the piece price all fall into place around it. Leave it out, and the shop is forced to guess, and a guessed volume returns a guessed price.
Guides
Each guide below takes one volume-economics question further than the overview above can — what the cost curve actually does at your order quantity.
- CNC machining company tolerances and surface finishes — what you can realistically expect, feature by feature and at volume.
- Aluminum CNC machining company economics — how the part’s cost falls from one piece to ten thousand, and which volume tier changes the math.
- Stainless steel CNC machining company economics — when the slow cut meets the volume curve — a cost structure that behaves differently from aluminum’s at every quantity.
- Aerospace CNC machining company economics — the volume that never comes — how to buy aerospace parts when no cost curve rewards quantity.
- Medical CNC machining company economics — when the volume arrives on a regulatory staircase — costing development, clinical, and launch batches separately.
- 5-axis CNC machining company economics — when the axis upgrade pays for itself at your quantity — treating the 5-axis choice as a quantity decision, not just a geometry one.
What this shop actually runs
A buyer asking for capability evidence should get a specific answer. The facility behind this guide operates 100+ CNC machines across a 6,800 m2 plant in Dongguan, China, with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Typical work: compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Typical work: prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Typical work: long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Typical work: shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Typical work: hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance bands held: ±0.003 mm on CNC milling, ±0.002 mm on CNC turning, ±0.002 mm on precision grinding and wire EDM. Capability indices: Ppk >= 1.67 initial on key characteristics; Cpk >= 1.33 ongoing in production.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded - disclosed openly), ISO 14001:2015 (116024/B/0001/UK/En). Certificates are issued to Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, established 2005).
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa. Based in China, serving customers worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Send your drawing for a quote.
Email [email protected] or call +86 13126536955 for a review and quote.
Frequently Asked Questions
What is your minimum order quantity?
Our MOQ is 1 piece. We take prototype and single-part orders as well as production runs, so you can validate a design before committing to volume.
Why do prototypes cost more per piece?
At low volume, the setup cost — programming, fixturing, and first-article inspection — is carried by a single part. At high volume that cost is amortized across thousands of parts. The lever is to reduce setups through design.
What dominates cost at high volume?
Once setup is amortized, cost is driven by cycle time, tool life, and yield. Process capability — Ppk ≥ 1.67 at the initial study on key characteristics — keeps cost predictable and scrap near zero at scale.
Where does setup stop mattering and cycle time take over?
In short, There is no single fixed point; it depends on the ratio of setup cost to per-piece cycle cost. When the setup is no longer a visible line on the unit price — usually once quantity passes the point where one more part costs more in machine time than the remaining setup share — cycle time, tool life, and scrap become the levers that matter.
How does material choice change the cost at volume?
In short, Material drives both the stock price and the machining speed. A free-machining grade cuts fast and holds tool life; a hard or work-hardening grade slows feeds and wears tools.
How do tolerances move the price?
In short, Tighter tolerances need more careful process control, more inspection, and sometimes an extra finishing step such as grinding. A drawing that calls out ISO 2768-m general tolerances costs less to make than one with tight positional callouts on every feature, so tolerance should be reserved for the features that actually need it.
Can I prototype and produce with the same supplier?
Yes. We run prototype and production on the same over a hundred machines under one quality system, so the process that made the prototype becomes the process that makes production, with no re-qualification hand-off.
What tolerances can you hold?
±0.003 mm on CNC milling, ±0.002 mm on CNC turning, and ±0.002 mm for precision grinding. We verify critical dimensions on Hexagon CMMs, with process capability Ppk ≥ 1.67 at the initial study on key characteristics.
Which materials do you machine?
In short, Aluminum, stainless steel, carbon and alloy steel, brass, copper, titanium, and magnesium, plus engineering plastics including ABS, POM, nylon, PTFE, and PEEK. Incoming lots are XRF-checked against the mill certificate so the grade you specify is the grade you receive.
How do I compare quotes at different volumes?
Ask each supplier to separate setup from piece price, name the process it assumes at your quantity, and state the material grade. Two quotes are only comparable when both break the cost down the same way and both price the identical drawing.
What happens on a reorder?
Your program, fixture, and inspection plan stay on file, so a reorder starts from the saved setup rather than a cold start. That keeps the per-part cost flat and the lead time short instead of charging you for the learning a second time.
How do I get a quote for the right volume?
Email your STEP, IGES, or 2D drawing to [email protected] with both the order quantity and the annual volume. We return a review and a quote matched to your actual volume, usually within one business day.
Do you use MIL-STD-105E or ANSI/ASQ Z1.4 sampling inspection?
In short, MIL-STD-105E is the U.S. military sampling inspection standard published in 1989; it specifies acceptable quality limit (AQL) sampling plans for lot-by-lot inspection.
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM A276/A276M-17 — Standard Specification for Stainless Steel Bars and Shapes
- ISO 9001 — Quality management systems — Requirements
CNC Machining Company Knowledge Base
Every dimension of cnc machining company a hardware buyer needs to qualify a supplier, verify a claim, or make a sourcing decision — organised by topic.
Factory & Certifications
Top 10 reasons to choose Zhuohang as your best CNC Machining Company
Buyers vet a CNC Machining Company on the same ten points, every time. Zhuohang answers each with something you can check — a plant, certificates, machine names and numbers.
- Start at one. The first article and the production run use one program and one datum set, which keeps the approved sample and the delivered part identical.
- Quote plus DFM in ~48 hours. The cost-lowering changes to your CNC Machining part are raised before machining begins, so there are no surprises at billing.
- A factory you can visit. Behind the parts is a 6,800 m² floor in Hengli, Dongguan, trading as Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39) since 2005.
- Customs-ready paperwork. Every order ships with material certificates, and we track the current US Section 301 / Section 232 and EU CBAM position for the HS codes we use.
- Real tolerances. ±0.003 mm milling, ±0.002 mm turning, ±0.002 mm grinding and wire EDM — measured to these, not merely quoted.
- Three certs, one system. ISO 9001:2015, IATF 16949:2016 (design excluded) and ISO 14001:2015 cover the same floor — prototype or automotive CNC Machining batch, one quality standard.
- Seven languages. English, Japanese, Portuguese, Spanish, French, Chinese and Cantonese — your drawing is answered in the language it was sent.
- No hand-offs. Milling, turning, mill-turn, grinding and wire EDM under one roof and one quality system, so CNC Machining parts stay in-house instead of stalling between suppliers.
- Machines you can name-check. Mazak VARIAXIS I-600, Mazak INTEGREX I-250H S, and Tsugami, Star and Citizen Swiss lathes — the gear behind tight features.
- SPC you can read. Every lot passes Hexagon CMM and vision checks, with Ppk ≥ 1.67 initial and Cpk ≥ 1.33 production figures, each noting index, stage and sigma method.
Fancy judging any of the ten for yourself? Send a drawing for a 48-hour quote, or reach the team in English, Japanese, Portuguese, Spanish, French, Chinese or Cantonese.